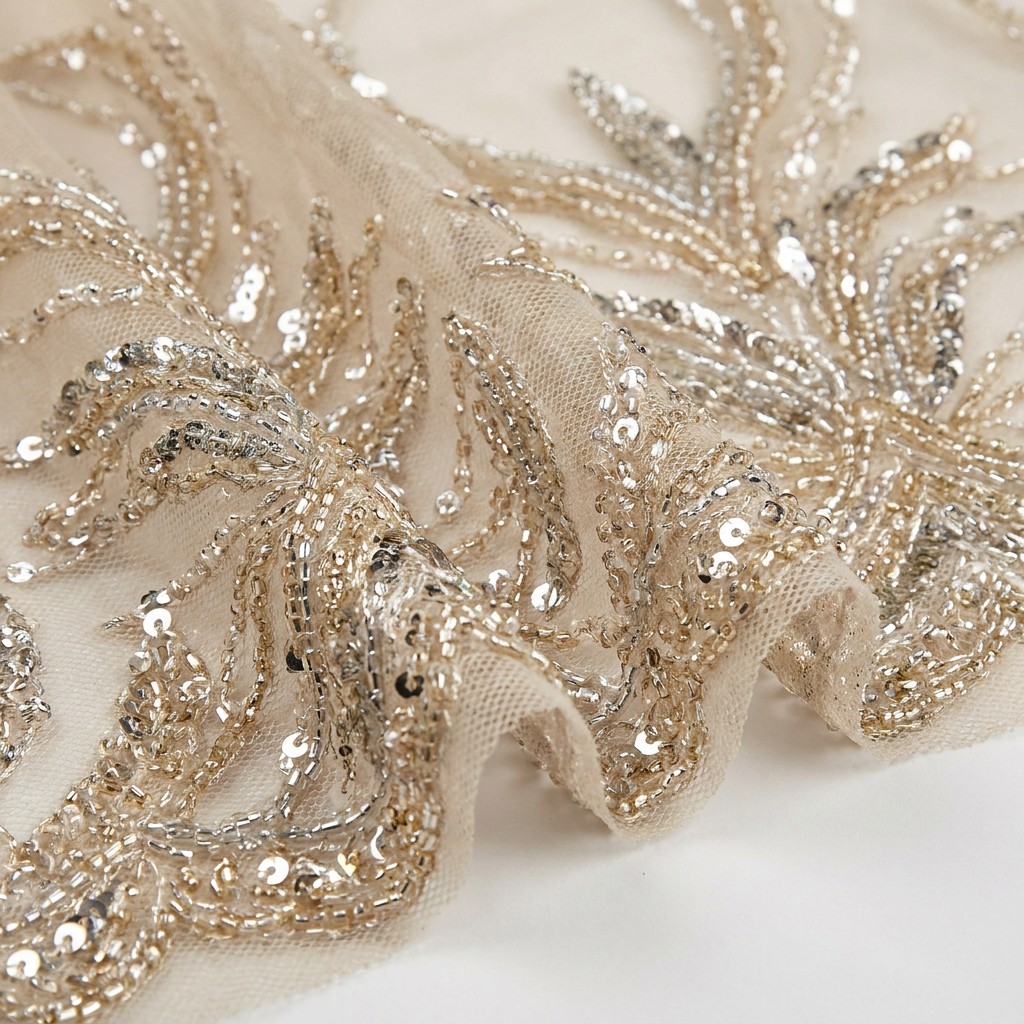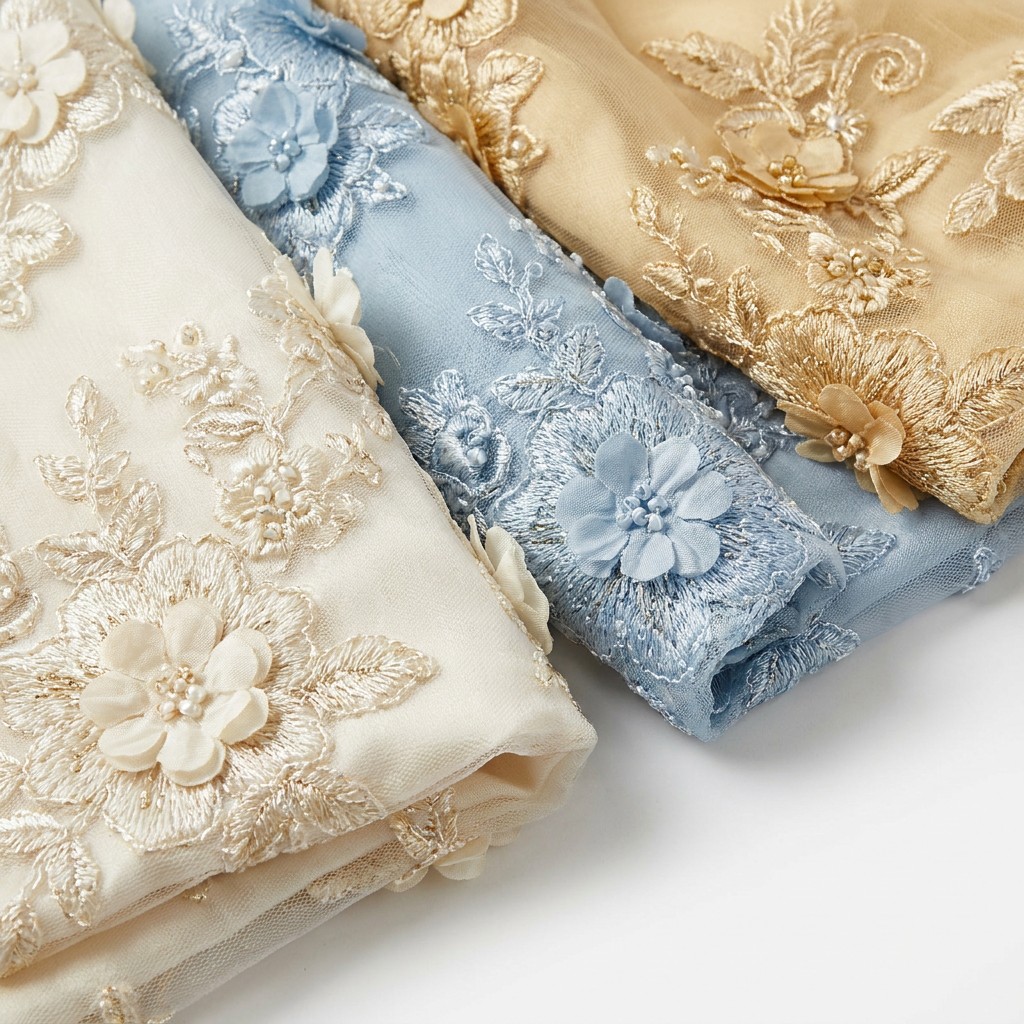
laser cut embroidery edge fraying for dependable B2B sourcing
laser cut embroidery edge fraying matters when a decorative fabric must look consistent, sew cleanly, and arrive ready for production. This guide explains the physical cause, factory controls, and inspection evidence that buyers can request from a specialist mill.
First, define the risk in measurable terms. Then connect the risk to a process setting and a release test. This gives designers, merchandisers, and quality teams one practical language for approval.
Why three-dimensional petals curl
A laser-cut floral applique combines organza, embroidery thread, adhesive, and sometimes foam or mesh. Heat softens synthetic fibres at the cut line. Uneven heating creates different shrinkage between face and backing.
Curling also increases when stitch density pulls the perimeter inward. A free edge has less support than the centre. Tune cutting and stitch sequence together.
Laser cut embroidery edge fraying at scale
A dull blade leaves fibres, but excess laser energy creates a hard or dark rim. The correct result is a clean sealed edge that preserves softness and colour.
Use the actual production stack for trials. Organza alone may cut cleanly, while metallic thread or adhesive reflects heat differently. Record lens, focus, speed, power, frequency, and air assist.
Pulse parameter development
Start with a low-energy trial matrix and increase energy in small steps. A shorter pulse or faster speed can reduce heat-affected width. Cooling between repeats prevents heat accumulation.
Check yellowing on pale organza, glazing on dark mesh, and brittleness on transparent film. Improve extraction and clean the lens when smoke deposits appear.
Removing burrs and melted decoration
A sealed edge should not feel sharp when lining passes across it. Hard burrs show excess energy, poor focus, or repeated passes. Adjust path rather than grinding the petal.
Keep beads, sequins, and metal threads outside the heat path. If decoration must sit close, approve a special parameter and inspect the reverse.
Backing and petal retention
Compatible backing can stabilise a petal during cutting and wear. It must release or remain flexible as required. Excess adhesive adds weight and creates a rigid fold line.
Test the complete applique after conditioning, steaming, and hanging. Measure petal radius, lift height, and edge curl at several points.
ISO 12947 abrasion screening
ISO 12947 Martindale testing can screen whether repeated contact damages the embroidered face and cut edge. Use a finished applique and define the endpoint.
Report load, abradant, cycles, conditioning, specimen location, and photographs. Visual grading should accompany cycle count for luxury garments.
Bridal and eveningwear application tests
A petal may rub against lining, skin, another petal, or a packing fold. Simulate garment movement with flex and fold tests. Check overlapping petals closely.
Steam and press a finished panel at approved temperature. Observe whether the petal returns to its lift without yellowing or flattening.
B2B petal inspection table
Inspectors should record edge width, colour, hardness, loose fibres, scorch marks, petal height, stitch security, adhesive bleed, and motif position.
Sample beginning, middle, and end of a roll. Isolate repeated hard edges or curl beyond tolerance and approve a replacement panel before continuing.
How B2B buyers set a repeatable specification
Start with a signed reference swatch, a technical data sheet, and a tolerance table. Record composition, usable width, GSM, construction, finish, colour code, roll length, and packing method. A clear specification lets production, inspection, and receiving teams measure the same result.
Next, approve a lab dip, strike-off, or development panel before bulk cutting. Keep one sealed approval sample with the purchase order. Then request an inline report, a final inspection report, and photographs of packed rolls. This sequence reduces disputes because every checkpoint has an owner and an acceptance rule.
MOQ, sampling, and production planning
Yunfan Textile supports a practical MOQ of 200 yards for these decorative fabric programs. Buyers can combine a confirmed colour, width, and construction with a realistic production window. Morris can advise on sample yardage, repeat placement, and the safest packing format for international delivery.
For a new design, reserve time for a first sample, a corrected sample when needed, and a pre-production approval. Allow extra time when the order includes special yarns, metallic effects, complex embroidery, or a custom finish. Clear approvals protect the buyer launch calendar and the factory production stability.
Inspection records that support confident sourcing
A useful B2B inspection sheet shows lot number, roll number, measured result, instrument, test method, inspector, and disposition. It also shows how defects are classified. Critical defects require rejection, major defects require a corrective action, and minor defects require a documented acceptance decision.
Ask the supplier to retain counter-samples from every approved lot. In addition, request images under consistent lighting and a short video of the material in motion. These records make remote approval more reliable and help your team compare future shipments with the original benchmark.
Sampling and communication checklist
- Confirm fibre content, width, GSM, usable area, and construction.
- State the colour reference, surface effect, backing, and intended end use.
- Define inspection method, tolerance, packing label, and roll identification.
- Approve a physical sample before the factory starts bulk production.
- Share delivery terms and contact Morris for a coordinated production plan.
For broader sourcing guidance, review the Quality Control category and the Sequin Fabric category. These internal resources help teams compare specifications, testing, and production controls before placing a purchase order.
Frequently asked questions for importers
Can I request a development sample? Yes. Share the target construction and end use with Morris so the team can confirm the most efficient sample route before the 200-yard production MOQ.
How should I approve colour? Approve a physical swatch under agreed lighting, record the reference number, and keep a signed control sample. A screen image alone cannot define a decorative surface accurately.
What should arrive with a bulk shipment? Request the packing list, roll map, final inspection report, relevant test results, and photographs showing labels and outer packaging.
Request a controlled development plan for laser cut embroidery edge fraying
Share your target application, construction, colour reference, width, and delivery window. Morris will help match the sample to the production route, explain the measurable tolerance, and confirm the 200-yard MOQ. A written approval protects your team from avoidable variation.
Source direct on Alibaba - request bulk pricing, specifications, and production details in one place.
View Yunfan Textile on AlibabaRequest Sequin Fabric Samples and share your target GSM, width, sequin size, and colour reference.
Talk to Morris directly:
Email: morris@yunfantextile.com
WhatsApp: +86 156 3752 5803
WhatsApp: +86 175 1619 6727

Implementation notes for a reliable decorative fabric program
Production teams benefit from a short control plan that connects the design brief to measurable factory actions. Begin with a physical reference, then list every variable that can change the result. These variables may include fibre, yarn, backing, coating, stitch density, machine speed, humidity, heat, storage time, and packing pressure. Assign each variable to a process owner and define the evidence required at approval.
Before bulk work starts, the factory should make a representative pilot panel. The pilot should include the most demanding motif, the most delicate edge, and the heaviest or densest area. Inspect the panel after conditioning and after the intended finishing operation. If the panel passes, keep it as a control sample. If it fails, record the failure mode and change only one process variable at a time.
Remote B2B approval works best when the photos, videos, and test reports use repeatable conditions. Use the same light source, camera distance, background, specimen direction, and scale. Show both the face and reverse. For dimensional checks, measure relaxed material rather than a piece held under tension. This discipline makes a supplier report useful to a product developer who is working in another time zone.
Buyers should also separate appearance acceptance from performance acceptance. A fabric can look correct but fail recovery, abrasion, seam stability, or packing simulation. Conversely, a technically strong fabric may need a small appearance adjustment before it suits a collection. Use a signed approval table with a clear disposition: accepted, accepted with note, rework required, or rejected.
After shipment, open a representative roll before releasing the whole order to cutting. Check label data, width, surface, hand, construction, and the most relevant test result. Record any difference from the control sample immediately. Early feedback allows the supplier to investigate the same lot and prevents a small issue from spreading across finished garments.
Finally, keep the control sample, inspection report, packing photographs, and corrective-action notes together with the purchase order. This file becomes a useful benchmark for repeat orders. It also helps both sides discuss facts instead of impressions. A consistent record supports faster quotations, more accurate production planning, and a more dependable customer delivery promise.