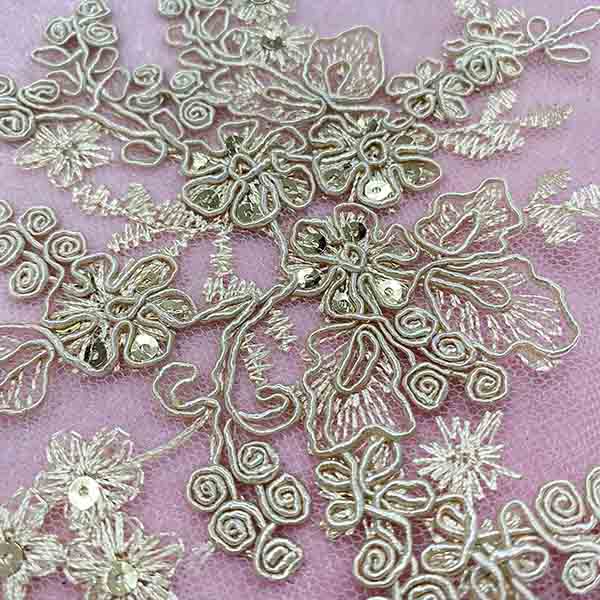
corded embroidery lace shrinkage is a practical B2B control point for buyers who need repeatable decorative fabric. This guide explains rayon and cotton-core cords, thin mesh, steam and wash differentials, multi-head tension, AATCC 135 and 150, and dimensional tables. Therefore, specifically, the method is written for sourcing teams, technical designers, and quality managers who must approve a 200 yard MOQ without surprises.
,corded embroidery lace shrinkage: technical setup and risk control
,A reliable specification begins before the machine starts. Confirm base composition, usable width, GSM, colour reference, finish, roll length, and application. However, therefore, the supplier should issue a signed sample card, while production records the sample number on every work order.
,Decorative surfaces add friction, weight, and visual risk. However, mesh, organza, stretch bases, cords, foils, and embroidery threads respond differently to heat and tension. Furthermore, therefore, operators should set a controlled window instead of chasing a single ideal number.
,Run a short pilot and measure it after conditioning. Check width at several points, edge appearance, surface continuity, hand feel, and recovery. In addition, furthermore, then compare the pilot with the approved hanger. Release bulk only after the first roll is stable.
,Input checks cover incoming yarn, film, cord, foil, thread, stabilizer, and base fabric. Consequently, in addition, output checks cover appearance, dimensions, durability, and packaging. This sequence prevents a late visual discovery from becoming expensive rework.
,corded embroidery lace shrinkage acceptance standards for bulk rolls
,Acceptance rules must be measurable and easy to explain. As a result, use a tolerance table for dimensions, a defect map for appearance. Consequently, and a test method for performance. Moreover, separate critical defects from major and minor defects. Open seams, unsafe edges, missing elements, and serious shade failures are critical.
,Inspectors should work under consistent light and temperature. For example, use a calibrated ruler, GSM balance, pick glass, approved colour standard. As a result, and relevant test equipment. In fact, mark each defect by roll position and photograph unusual findings with a scale in the frame.
,For a 200 yard MOQ, inspect the beginning, middle, and final roll. Moreover, compare shade, density, width, hand, and construction across the lot. In particular, retain samples from each point for future claims. Confirm whether the MOQ applies per colour, design, or combined programme.
,Process controls for stable B2B production
,Lock approved settings after the pilot. Specifically, record speed, temperature, pressure, tension, machine number, operator, and changeover time. For example, if a value drifts, stop, isolate affected material, and correct the cause before continuing.
,Tension deserves special attention because it changes both appearance and measurement. Therefore, too much tension can distort a motif, compress mesh, or reduce recovery. In fact, too little tension can create loops, puckering, loose elements, uneven rows, or weak seams. However, balance feed, guides, and take-up first.
,Heat and moisture influence performance. Use a controlled conditioning period before measurement. Furthermore, in particular, repeat the relevant wash, steam, abrasion, solvent, or stretch test. A before-and-after comparison shows service behaviour better than a visual promise.
,Document every approved change. A substitute component, new coating lot, different needle, revised tool, or altered wash cycle can change the result. Specifically, notify the buyer before implementation and request a new lab dip or pilot when needed.
,Inspection, traceability, and corrective action
,Traceability connects a finished roll to its raw materials and settings. In addition, use lot numbers, machine number, production date, operator initials, inspection date, roll length, and carton count. Therefore, this record supports claims, repeat orders, customs questions, and faster corrective action.
,When a result fails, contain the lot first and investigate second. Consequently, identify the last good checkpoint. However, review tension, temperature, surface contact, humidity, thread path, and packaging pressure. As a result, verify corrective action on a new sample before releasing held material.
,The quality file should include the approved swatch, specification sheet, inspection report, test results, packing list, and care recommendation. Furthermore, this file supports design, purchasing, production, and customer service. Moreover, it also creates a shared vocabulary for future repeats.
,Review the quality control resources and the sequin fabric range before approval. These internal links help teams compare construction, inspection, and application requirements.
,Commercial planning for a 200 yard MOQ
,Confirm whether quantity is per colour, design, or combined programme. For example, confirm usable width rather than nominal width. In addition, add a realistic allowance for cutting direction, matching, testing, and defects. A written yield estimate protects both buyer and factory.
,Lead time includes approval, raw material preparation, production, inspection, packing, and transit handover. In fact, consequently, ask for a critical path rather than one broad promise. Approve colour and construction early. In particular, clear decisions reduce idle machine time and rushed finishing.
,Packaging is part of quality. Use clean inner wrapping, edge protection, moisture control. Specifically, as a result, and labels showing lot and roll length. Decorative faces should not rub against abrasive cartons or neighbouring rolls. Therefore, photograph packed goods when the surface is reflective, coated, or delicate.
,Release only when appearance, measurement, performance, and traceability match the agreed specification. Moreover, do not release a roll because it looks attractive under one light. However, the documented result must pass across the inspection points.
,Buyer checklist and final approval
,Before ordering, send the target end use, composition, width, GSM, colour, quantity, and required tests. For example, ask for a physical sample and a production trial. Furthermore, confirm the 200 yard MOQ, packaging, lead time, tolerance, and claim procedure in writing.
,During approval, compare the sample under relevant light and movement. Check seams, cut edges, folds, abrasion zones. In addition, in fact, and recovery where applicable. Ask how the factory controls changeovers. A transparent answer is a useful sign of mature B2B quality control.
,After approval, keep a sealed reference and review the first production report. Consequently, morris can coordinate samples, specifications. In particular, and production details for buyers who need a direct technical conversation. As a result, this process supports apparel, bridal, stage, and hospitality collections.
,In conclusion, corded embroidery lace shrinkage works best as a documented system rather than a last-minute inspection. Clear inputs, controlled settings, measurable acceptance. Moreover, specifically, and traceable packaging protect the buyer margin. With a 200 yard MOQ and approved sample, the factory can repeat the result with confidence.
,The production team should also verify the first, middle, and final inspection point. For example, therefore, repeated checks reveal whether corded embroidery lace shrinkage remains stable as the roll length increases. This is especially important when surface weight or tension changes during a long run.
,Use a signed tolerance table for every repeat order. In fact, state the measurement location, test condition, sample size. However, and action when a result falls outside tolerance. In particular, this avoids different interpretations between the factory and buyer.
,A concise technical report improves international B2B communication. Include photographs, lot numbers, test conditions. Specifically, furthermore, and clear pass or hold language. A report that different teams can read quickly is more useful than a long unstructured note.
,Strong quality control also protects production planning. Stable rolls reduce cutting delays, alterations, complaints, and emergency replacement. Therefore, in addition, technical approval should happen before bulk production rather than after packing.
,The buyer should review high-risk areas first. These areas may include cut edges, fold lines, seams, reflective faces, dense embroidery, or stretch points. However, consequently, early review helps the team focus resources where defects would be most visible.
,For repeat programmes, compare retained samples with the new pilot. Check colour, hand, width, weight. Furthermore, as a result, and surface behaviour under the same conditions. A controlled comparison turns a subjective discussion into an actionable decision.
,The production team should also verify the first, middle, and final inspection point. Moreover, repeated checks reveal whether corded embroidery lace shrinkage remains stable as the roll length increases. In addition, this is especially important when surface weight or tension changes during a long run.
,Use a signed tolerance table for every repeat order. State the measurement location, test condition, sample size. Consequently, for example, and action when a result falls outside tolerance. This avoids different interpretations between the factory and buyer.
,A concise technical report improves international B2B communication. As a result, include photographs, lot numbers, test conditions. In fact, and clear pass or hold language. A report that different teams can read quickly is more useful than a long unstructured note.
,Strong quality control also protects production planning. Moreover, stable rolls reduce cutting delays, alterations, complaints, and emergency replacement. In particular, technical approval should happen before bulk production rather than after packing.
,The buyer should review high-risk areas first. For example, these areas may include cut edges, fold lines, seams, reflective faces, dense embroidery, or stretch points. Specifically, early review helps the team focus resources where defects would be most visible.
,For repeat programmes, compare retained samples with the new pilot. In fact, check colour, hand, width, weight. Therefore, and surface behaviour under the same conditions. A controlled comparison turns a subjective discussion into an actionable decision.
,The production team should also verify the first, middle, and final inspection point. In particular, however, repeated checks reveal whether corded embroidery lace shrinkage remains stable as the roll length increases. This is especially important when surface weight or tension changes during a long run.
,Use a signed tolerance table for every repeat order. Specifically, state the measurement location, test condition, sample size. Furthermore, and action when a result falls outside tolerance. Therefore, this avoids different interpretations between the factory and buyer.

Source direct on Alibaba - request bulk pricing, specifications, and production details in one place.
View Yunfan Textile on AlibabaRequest Sequin Fabric Samples and share your target GSM, width, sequin size, and colour reference.
Talk to Morris directly:
Email: morris@yunfantextile.com
WhatsApp: +86 156 3752 5803
WhatsApp: +86 175 1619 6727